


Latest Post
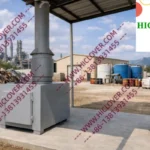
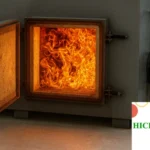
Elevating Waste Management: HICLOVER Waste Incinerators for Municipal and Small Waste Treatment
Elevating Waste Management: HICLOVER Waste Incinerators for Municipal and Small Waste Treatment
The Necessity of Advanced Waste Incineration Solutions
As cities and industries expand, the challenge of managing municipal waste has become increasingly complex. The introduction of the waste incinerator for municipal waste presents a viable solution, especially considering the stringent environmental regulations imposed by global authorities like the WHO and EU emission frameworks. HICLOVER’s waste incinerators are engineered to operate within rigorous industrial standards, maintaining combustion temperatures between 850°C to 1,100°C, ensuring complete waste destruction. This technical reliability is crucial for minimizing environmental impact while maximizing efficiency in waste management processes.
The HICLOVER Advantage: Engineering Excellence and Market Positioning
HICLOVER’s market positioning stems from over 16 years of experience in the waste management sector. The brand is recognized for its engineering excellence in manufacturing incinerators for small waste incinerators and larger municipal systems. HICLOVER integrates advanced technologies such as PLC automation, ensuring efficiency in operations and safety in management. The brand’s engineering experience allows for customizable chamber volumes, adapting to various waste disposal needs, whether for centralized municipal systems or decentralized setups required in remote mining and oil camps.
Innovative Design Features
The HICLOVER waste incinerator incorporates essential features that enhance safety and operational efficiency. Dual combustion chambers are utilized to optimize the incineration process, ensuring that waste is subjected to high temperatures for adequate retention. High-temperature retention is pivotal in achieving complete combustion, which significantly reduces harmful emissions. Additionally, optional wet or dry scrubbers are available, further minimizing the environmental footprint. These safety features ensure compliance with international standards while delivering high-performance waste management solutions.
Types of HICLOVER Waste Incinerators
When considering waste disposal technologies, a comparison between fixed and containerized incinerators reveals significant advantages in flexibility and adaptability. HICLOVER’s containerized modular systems allow for mobile plug-and-play designs that can be deployed in various locations, essential for disaster relief efforts in crisis zones and humanitarian camps. The capacity to quickly set up a waste management solution in such areas underscores HICLOVER’s commitment to global infectious disease preparedness and environmental responsibility.
Addressing Regulatory Compliance and Safety Standards
Ensuring compliance with safety standards is crucial for any waste management operation. HICLOVER’s waste incinerators are designed to meet and exceed both national and international regulations, with a focus on ESG compliance. This commitment to sustainability not only enhances the brand’s reputation but also aligns with growing societal pressure to adopt environmentally responsible practices. By integrating advanced technology, HICLOVER provides an efficient, reliable, and safe solution for waste incineration, reinforcing governmental priorities in waste management policies.
Operational Efficiency: PLC vs. Manual Control Systems
HICLOVER’s incorporation of PLC-controlled systems significantly improves the operational efficiency of waste management processes. These automated systems reduce the potential for human error, enhance safety features, and ensure consistent performance. In contrast, manual control systems can lead to variability in operations and increased safety risks. The adoption of PLC technology allows HICLOVER to maintain a stable supply chain and meet the demands of diverse industries, from healthcare to municipal waste management.
Energy Recovery: A Sustainable Approach
With the increasing focus on carbon emission reduction, HICLOVER’s waste incinerators are designed with energy recovery systems. This technology not only aids in reducing the environmental impact but also contributes to energy efficiency, transforming waste into renewable energy resources. The ability to harness energy from waste aligns with current sustainability trends, which are becoming paramount in global waste management discussions.
Global Reach and Customization Options
HICLOVER boasts a robust global export capability, enabled by a stable supply chain and long-standing manufacturing experience. Their factory direct supply model allows for tailored solutions, addressing the specific needs of different regions and regulatory requirements. Providing customizable waste incinerators ensures that local governments and regulatory bodies can confidently implement HICLOVER solutions in a way that aligns with their operational goals and environmental expectations.
Benefits for Government Officials and Regulatory Bodies
Implementing HICLOVER waste incinerators empowers government officials and regulatory bodies to manage municipal waste effectively while adhering to environmental regulations. The engineering reliability, dual combustion chamber technology, and energy recovery capabilities provide a comprehensive waste management solution. Moreover, the emphasis on safety features and compliance ensures that local regulations are met, ultimately fostering public trust in waste management initiatives.
For more information on HICLOVER’s innovative waste management solutions and to explore collaboration opportunities, visit HICLOVER’s website.
Conclusion: The Future of Waste Management with HICLOVER
Investing in HICLOVER waste incinerators represents a forward-thinking approach to waste management. By combining advanced engineering, regulatory compliance, and a commitment to sustainability, HICLOVER stands at the forefront of the waste disposal industry. As the world shifts towards decentralized waste management and innovative waste treatment technologies, HICLOVER will continue to lead the way in providing effective solutions that meet the needs of governments and regulatory bodies worldwide.
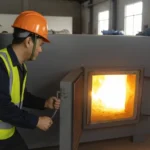
HICLOVER Waste Incinerators: Engineering Reliability and Global Market Leadership in Waste Management
HICLOVER Waste Incinerators: Engineering Reliability and Global Market Leadership in Waste Management
1. Technical Overview and Temperature Standards
Waste incineration is a proven method of disposing of medical, industrial, and animal waste. HICLOVER waste incinerators comply with industrial standards, operating within a temperature range of 800-1000°C, ensuring efficient waste destruction and environmental responsibility. Leveraging over 16 years of engineering experience, HICLOVER waste incinerators prioritize technical clarity, precision, and reliability. Learn more about temperature standards.
2. Combustion Principles and Dual Chamber Explanation
HICLOVER waste incinerators employ advanced combustion principles to maximize waste destruction while minimizing emissions. The dual-chamber design is essential for proper waste incineration. In the primary chamber, waste is reduced to ash and gases. The secondary chamber further breaks down harmful gases before releasing them into the atmosphere, ensuring emissions remain within regulatory limits.
3. Regulatory Compliance: WHO, EU, and Other Frameworks
HICLOVER waste incinerators adhere to strict regulations, including guidelines set by the World Health Organization (WHO) and the European Union. These incinerators meet and exceed local, national, and international standards, ensuring safe and environmentally responsible waste disposal. By investing in HICLOVER products, customers can be confident in their compliance with waste management regulations.
4. Comparing Incinerator Types: Fixed vs. Containerized
Fixed waste incinerators are permanent installations, best suited for long-term, centralized waste management solutions. HICLOVER’s containerized mobile incinerators offer versatility, allowing customers to transport and deploy the units as needed. This mobility is particularly useful in crisis zones, humanitarian camps, remote mining/oil camps, and decentralized waste management scenarios.
5. PLC vs. Manual Control and Automation Advantages
HICLOVER waste incinerators can be equipped with PLC-controlled automation systems, streamlining waste management tasks. PLC-controlled incinerators offer improved efficiency, safety, and reliability compared to manual controls. To learn more about the benefits of PLC-controlled waste incinerators, visit HICLOVER’s website.
6. Dry Scrubber vs. Wet Scrubber and Emission Reduction
Both dry and wet scrubbers are designed to remove pollutants from waste incinerator emissions. Dry scrubbers use a dry powder to neutralize acidic gases, while wet scrubbers utilize a liquid to achieve the same result. HICLOVER waste incinerators provide customizable emission treatment options tailored to customers’ unique requirements. Contact HICLOVER for more information.
7. Factory Manufacturing and Supply Chain Stability
HICLOVER manufactures waste incinerators directly, ensuring factory-direct supply, customizable chamber volumes, and global export capabilities. With a stable supply chain and extensive engineering experience, HICLOVER waste incinerators provide reliable waste management solutions for customers worldwide.
8. Integrating Modern Trends: Global Infectious Disease Preparedness
HICLOVER waste incinerators support global infectious disease preparedness by offering reliable, cost-effective waste disposal for medical facilities. As the world confronts new health challenges, HICLOVER remains committed to providing advanced waste management solutions that protect communities and the environment.
9. Carbon Emission Reduction and ESG Compliance
HICLOVER waste incinerators comply with Environmental, Social, and Governance (ESG) standards by reducing carbon emissions and promoting sustainable waste management practices. Investing in HICLOVER products contributes to a greener, more responsible future.
10. Decentralized Waste Management and Energy Recovery Systems
Decentralized waste management offers an efficient, eco-friendly alternative to traditional waste management systems. HICLOVER waste incinerators, equipped with energy recovery systems, can convert waste heat into electricity, reducing overall energy consumption and promoting sustainable waste management practices.
11. Digital Automation in Industrial Equipment
HICLOVER’s PLC-controlled waste incinerators incorporate digital automation, streamlining waste management tasks and ensuring consistent performance. By harnessing the power of digital automation, HICLOVER waste incinerators enhance efficiency, safety, and reliability.
HICLOVER waste incinerators offer advanced engineering, global market leadership, and unparalleled waste management solutions. Trust HICLOVER for reliable, sustainable waste management, setting the standard for excellence in waste disposal.
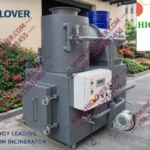
HICLOVER TS-30D PLC Incinerator (Former YD-30 PLC): Intelligent Small-Scale Waste Incineration Solution
HICLOVER TS-30D PLC Incinerator (Former YD-30 PLC): Intelligent Small-Scale Waste Incineration Solution
The HICLOVER TS-30D PLC incinerator, previously known as YD-30 PLC, is a compact, fully automatic waste incineration system designed for facilities that require stable high-temperature destruction, operator safety, and fuel-efficient operation. With a nominal burn rate of 30 kg per hour, the TS-30D PLC is optimized for medical, laboratory, small industrial, and institutional waste disposal where compliance, reliability, and controlled emissions are critical.
Built on HICLOVER’s long-established incinerator design philosophy, the TS-30D PLC combines traditional refractory engineering with modern PLC automation, ensuring consistent performance under continuous operation.
Designed for Controlled and Safe Waste Destruction
The TS-30D PLC adopts a dual-chamber high-temperature configuration with adjustable high-temperature retention (HTR). The system ensures complete oxidation of waste and flue gases while minimizing operator exposure and environmental risks.
-
Average burn rate: 30 kg/hour
-
Feed mode: Manual feeding with intelligent operator protection
-
Continuous operation logic supported by PLC automation
-
Automatic burner ignition and shutdown
The intelligent sensor system enables continuous feeding logic while preventing unsafe access during operation, reinforcing worker protection standards.
Dual-Chamber High-Temperature Combustion System
Primary Combustion Chamber
-
Volume: 330 L
-
Internal dimensions: 75 × 75 × 60 cm
-
Operating temperature: 800 ℃ – 1000 ℃
-
Hot face refractory:
-
Thickness ≥ 115 mm
-
≥ 65 % Al₂O₃
-
1750 ℃ grade
-
-
Cold face insulation: High-grade refractory ceramic fiber
Secondary Combustion Chamber
-
Volume: 180 L
-
Operating temperature: 1000 ℃ – 1300 ℃
-
Gas residence time: ≥ 2.0 seconds
-
Mix combustion chamber ensures uniform gas turbulence and complete oxidation
This configuration is suitable for pathological waste, infectious materials, pharmaceutical residues, and small-volume hazardous waste.
PLC Automatic Control and Intelligent Monitoring
The TS-30D PLC is equipped with a PLC automatic control system with LCD interface, enabling precise control, monitoring, and diagnostics.
Key control features include:
-
Real-time temperature monitoring with corundum probe tube (rated up to 1400 ℃)
-
Progress display bar and time visualization
-
Programmable time settings
-
System self-testing mode
-
Automatic false alarm detection
-
Automatic protection operator (APO) logic
-
Automatic cooling cycle after shutdown
The PLC system reduces dependence on operator experience and improves long-term operational stability.
Fuel Efficiency and Burner Configuration
The TS-30D PLC is designed with intelligent fuel-saving logic, optimizing burner operation based on chamber temperature feedback.
-
Burner type: Italy brand
-
Fuel options:
-
Diesel oil (standard)
-
Natural gas (optional configuration)
-
-
Diesel consumption: ~10 kg/hour
-
Burner operation: Fully automatic ON/OFF
This approach balances combustion stability, fuel economy, and equipment longevity.
Integrated Flue Gas Treatment Options
To meet diverse environmental requirements, the TS-30D PLC includes a dry smoke filter chamber as standard.
-
Dry scrubber: Included
-
Wet scrubber: Optional (site-specific emission control)
-
Chimney height: 5 meters
-
Chimney material: Stainless Steel 304
This modular approach allows adaptation to local emission standards without over-engineering.
Mechanical Structure and Feeding Options
-
Feeding door options:
-
Side / front loading: 55 × 50 cm
-
Top loading (optional): 75 × 75 cm
-
-
External dimensions (main body): 175 × 120 × 140 cm
-
Gross weight: ~3500 kg
-
Sealing material: Refractory ceramic fiber
-
Exterior paint: 250 ℃ high-temperature resistant coating
An upgrade to containerized mobile type is available for remote or temporary installations.
Electrical and Utility Requirements
-
Voltage: 220 V
-
Installed power: 0.7 kW
-
Oil tank capacity: 200 L
-
Oil tank stand: Included
-
Liquid level display: Standard
Low electrical demand makes the TS-30D PLC suitable for areas with limited infrastructure.
Certifications and Compliance
The TS-30D PLC is manufactured under certified quality and compliance systems:
-
CE certification:
-
2006/42/EC
-
2014/30/EU
-
-
ISO certification: ISO 9001:2015
-
High-Tech Enterprise Certification: Yes
These certifications support international procurement, institutional buyers, and regulated markets.
Typical Application Scenarios
The HICLOVER TS-30D PLC incinerator is well suited for:
-
Hospitals and clinics
-
Laboratories and research centers
-
Veterinary facilities
-
Quarantine stations
-
Small industrial waste treatment points
-
Remote or decentralized waste management sites
Its balance of traditional refractory durability and forward-looking PLC automation makes it a dependable long-term asset.
Conclusion
The HICLOVER TS-30D PLC incinerator represents a refined evolution of the YD-30 PLC platform, offering stable high-temperature combustion, intelligent control, and flexible emission treatment in a compact footprint. It is a practical solution for facilities seeking reliable small-scale incineration with modern safety and efficiency standards.
For technical inquiries or configuration options, visit www.hiclover.com or contact [email protected].